


Polypropylene Applications: Industrial Uses, Grade Selection, and Manufacturing Methods
Published on Monday, 26. October 2026
Content Guide:Discover key polypropylene applications and engineering properties. Learn how to select the right PP grade and choose between CNC machining and molding. A practical engineering guide to polypropylene applications. Compare PP grades, review chemical resistance, and learn how to manufacture custom PP
Polypropylene (PP) is a lightweight thermoplastic used in packaging, fluid-handling systems, vehicles, laboratory equipment, consumer products, fibers, and industrial components. The right choice depends on the specific PP grade, the service environment, and the manufacturing process.
PP applications
Grade selection
Manufacturing methods
B2B procurement
Quick answer
Where is polypropylene used? Common polypropylene applications include food and industrial packaging, automotive interior and under-hood components, chemical tanks, laboratory supplies, healthcare products, electrical insulation, pipe systems, and custom machined machine components.
Why choose PP? It combines low weight, resistance to many aqueous chemicals, low moisture uptake, and broad processing options. Its limitations include creep under sustained load, temperature-dependent stiffness, and poor UV resistance without stabilizing additives.
How should engineers choose a process? Injection molding suits repeatable, high-volume complex parts; extrusion suits continuous profiles and sheets; thermoforming suits sheet-based shapes; and CNC milling or turning is ideal for prototypes, low-volume parts, and custom geometries.
EnvironmentCheck continuous operating temperature, chemical concentrations, UV exposure, and cleaning agents.
Mechanical designReview stiffness, cold-temperature impact, creep under load, and dimensional stability.
Production planBalance order volume against tooling cost, design changes, finish, tolerance, and inspection needs.
What Is Polypropylene?
Properties that shape applications
Major industrial applications
Choosing a PP grade
Choosing a manufacturing process
PP vs. other plastics
Common selection mistakes
Procurement checklist
Frequently asked questions
References and fact check
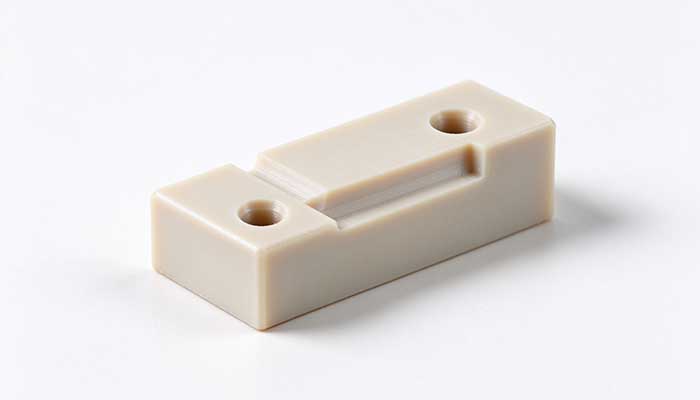
Polypropylene, abbreviated PP, is a thermoplastic polyolefin made by polymerizing propylene. It is a semi-crystalline plastic available in multiple formulations for both flexible and rigid products. Its broad use reflects a useful balance of weight, chemical resistance, processability, and cost.
PP is not one interchangeable material. Homopolymer, random copolymer, and impact copolymer grades differ in stiffness, cold-temperature impact performance, clarity, and processing behavior. Fillers, reinforcing glass fibers, pigments, UV stabilizers, and flame-retardant packages can further alter performance.
For design and purchasing, specify the actual grade (or a supplier-approved equivalent) rather than writing "polypropylene" generically on a drawing. Confirm the selected grade’s datasheet, available stock form, and any regulatory documentation required by the end use.
When screening PP for an application, engineers must review both its strengths and its thermal/mechanical limitations. For reference, while PP melting points generally range from 130°C to 171°C depending on the formulation, continuous service temperatures usually max out around 80°C to 100°C for unloaded parts.
How PP material behavior affects engineering decisions | |||
Property or behavior | Potential engineering benefit | Application example | Limitation or design check |
|---|---|---|---|
Chemical resistance | Tolerates a range of aqueous acids, alkalis, salts, and process fluids. | Tanks, ducts, and chemical-handling components. | Compatibility varies with concentration and temperature. Oxidizing acids and certain halogens can degrade PP. |
Low moisture absorption | Limits moisture-driven dimensional changes compared to nylons. | Wet-process fixtures and laboratory items. | Thermal expansion still affects dimensions; low moisture uptake does not guarantee absolute precision. |
Fatigue behavior | Excellent flexural fatigue life in well-designed hinges. | Living hinges, flip-top closures, clips. | Hinge geometry and molecular orientation during injection molding are critical. Does not apply well to CNC-machined hinges. |
Low surface energy | Resists adherence of unwanted substances; easy to clean. | Food bins, guides, covers. | Makes adhesive bonding, printing, and painting very difficult. Requires surface prep (corona, plasma, flame) or welding to join. |
Electrical insulation | High dielectric strength for dry or controlled environments. | Cable components, electrical enclosures. | Confirm the required temperature rating, flame behavior, and relevant electrical standards for the specific grade. |
Creep and thermal expansion | Lightweight parts can be economical if loads are small. | Spacers, covers, supports, brackets. | Long-term stress causes cold flow (creep). Must use generous support, appropriate geometry, and realistic tolerances. |
UV and weathering | Stabilized grades survive defined outdoor exposures. | Agricultural fittings, irrigation components. | Standard, unstabilized PP degrades rapidly (chalking, embrittlement) under UV exposure. |
PP serves both high-volume consumer products and custom industrial parts. These are screening examples; another plastic or metal may be better for high wear, extreme precision, or severe loads.
Typical parts: tanks, fittings, pipe sections, ducts, pump housings, and manifolds. Why PP: Resistance to many aqueous process chemicals without rusting. Processes: extrusion, molding, fabrication (hot gas welding), and CNC machining. Check: exact chemical mixture, temperature, and pressure.
Typical parts: trim, interior panels, ducts, battery cases, and under-hood clips. Why PP: Low mass, vibration dampening, and a broad range of glass-filled/compounded grades. Processes: injection molding. Check: heat aging, impact requirements, and emissions.
Typical parts: trays, containers, sample holders, fixtures, and spacers. Why PP: Low moisture uptake and resistance to laboratory liquids and repeated washing. Processes: molding for high volume; CNC machining for custom geometries. Check: sterilization temperatures (autoclaving may warp some grades).
Typical parts: caps, closures, tubs, trays, and living hinges. Why PP: low weight, moldability, and flexural fatigue resistance. Processes: injection molding, extrusion, and thermoforming. Check: seal design, cold-temperature impact, and food-contact compliance.
Typical parts: selected trays, housings, syringes, and sample containers. Why PP: specialty grades are formulated for defined sterilization needs (e.g., radiation, EtO). Processes: molding and extrusion. Check: biological evaluation, sterilization cycles, and regulatory traceability.
Typical parts: bins, covers, guides, and contact containers. Why PP: easily cleaned, low moisture absorption, and resistance to aggressive food-facility sanitizers. Processes: molding, extrusion, and machining. Check: specific food-contact compliance for the exact grade (e.g., FDA/EU guidelines).
Typical parts: guards, spacers, brackets, blocks, and manifolds. Why PP: Easy to machine from stock materials without dedicated mold tooling. Processes: CNC milling or turning. Check: deflection under load, achieving tight tolerances, and thread pull-out strength.
The grade family gives a starting point, but not a complete specification. Resin suppliers offer individual grades optimized for extrusion, impact, transparency, stiffness, or sterilization.
Typical PP grade-family trade-offs | ||
Grade family | Typical benefits | Crucial limitations |
|---|---|---|
PP homopolymer | High stiffness, high tensile strength, favorable strength-to-weight ratio. Good for rigid parts. | Becomes brittle and susceptible to impact failure near or below 0°C (32°F). |
PP random copolymer | Improved clarity, flexibility, and a different stiffness/impact balance. | Does not achieve glass-like transparency; structural rigidity is lower than homopolymer. |
PP impact (block) copolymer | Contains elastomer components specifically designed to survive cold-temperature impact. | Lower overall stiffness and lower continuous operating temperatures than homopolymer. |
Filled / reinforced PP | Glass fibers or minerals (talc) improve stiffness, dimensional stability, and heat deflection. | Increases weight (density), causes tool wear during CNC machining, and creates anisotropic properties. |
Comparison of common PP manufacturing methods | |||
Process | Best-fit scenarios | Advantages | Key trade-offs |
|---|---|---|---|
Injection molding | High-volume 3D parts with stable geometry (e.g., automotive clips, caps). | Excellent repeatability and low per-part cost at scale; can form living hinges. | High upfront tooling cost; design revisions are expensive after the mold is cut. |
Extrusion | Continuous products like film, pipe, profiles, and sheet stock. | Highly efficient for continuous cross-sections. | Limited strictly to constant-profile geometries. |
Thermoforming | Trays, panels, covers, and large sheet-based shapes. | Lower tooling complexity and cost than large injection molds. | Struggles with wall thinning, deep draws, and requires secondary trimming. |
CNC milling & turning | Prototypes, low-volume custom parts, manifolds, and thick fixtures. | Zero mold tooling cost; easily accommodates design revisions; fast lead times. | Material removal is slow; PP's compliance makes tight tolerances difficult. |
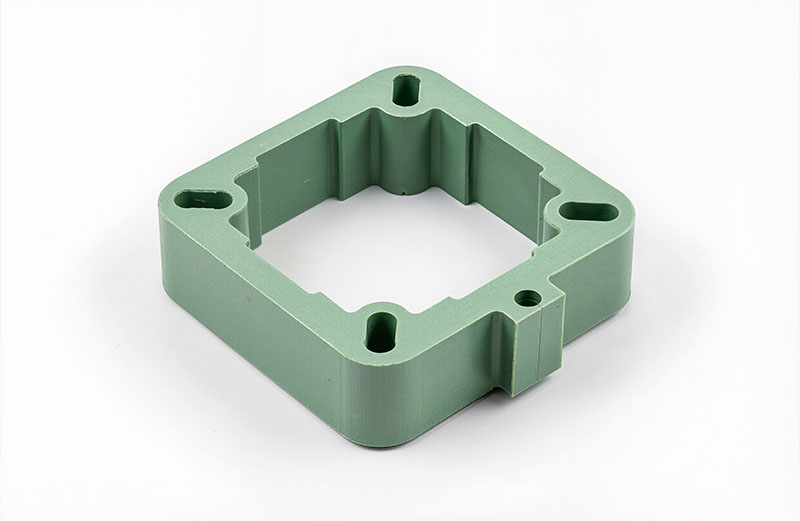
CNC machining is highly effective for custom chemical-handling blocks, laboratory fixtures, spacers, and custom manifolds made from standard PP plate or rod. However, PP requires specific machining strategies:
Heat sensitivity: PP will melt or smear if cutting speeds and feeds generate too much friction. Sharp, high-positive rake tooling and adequate coolant (or cold air) are necessary.
Elastic recovery: PP is compliant. It can flex away from the cutting tool and "spring back," meaning tightly toleranced holes may end up undersized.
Chip control: PP tends to form long, continuous, stringy chips that can wrap around tooling, requiring programmed chip-breaking routines.
Tolerances: Do not specify extremely tight tolerances (e.g., ±0.001") on a CAD model unless absolutely critical. Discuss achievable limits with your machinist, as PP is subject to thermal expansion and stress relief post-machining.
Compare actual datasheets against your specific load case. No material below is universally superior to PP.
Practical comparison for early material screening | ||
Material | Typical strengths vs. PP | Limitations vs. PP |
|---|---|---|
HDPE | Superior low-temperature impact toughness; slightly better resistance to some solvents. | Generally less stiff than PP homopolymer; lower continuous heat resistance. |
ABS | Better dimensional stability, easier to glue/paint, excellent room-temperature impact. | Poor chemical resistance to solvents and organics; lower fatigue resistance. |
POM (Acetal/Delrin) | Much higher stiffness, excellent machinability, extremely low friction and wear. | Higher density (heavier), vulnerable to strong acids, higher raw material cost. |
Nylon (PA) | Incredible mechanical strength, heat resistance, and wear characteristics. | Absorbs moisture, which causes parts to swell and lose dimensional accuracy. |
Common mistake | Why it causes problems | How to avoid it |
|---|---|---|
Assuming all PP resists cold impacts | Homopolymers become brittle near freezing temperatures. | Specify impact block copolymers for sub-zero environments. |
Ignoring operating temperature | Stiffness and load capacity drop significantly as temperatures approach 80°C+. | Record continuous and peak temperatures against the specific grade's heat deflection data. |
Underestimating thermal expansion | PP expands with heat more than metals; long parts may warp or bind. | Design in expansion gaps; use generous tolerances for long spans. |
Using unstabilized PP outdoors | UV rays break down the polymer chains, causing chalking and cracking. | Specify UV-stabilized formulations or carbon-black additives for outdoor use. |
Assuming food/medical compliance | Compliance depends on additives, mold release agents, and factory conditions. | Obtain explicit FDA, USP Class VI, or ISO 10993 documentation for the exact batch. |
Before issuing a purchase order for custom PP components, align engineering, quality, and procurement on the following parameters to avoid receiving non-compliant parts:
Exact material specification: State the exact grade/family (e.g., PP Homopolymer, 30% Glass-Filled PP), required color, and explicitly state if a "proposed equivalent" is allowed.
Chemical and thermal exposure: Document every process fluid, cleaner, concentration percentage, and peak operating temperature the part will face.
Documentation & compliance: For regulated industries, require Material Test Reports (MTRs), traceability records, and applicable food-contact or healthcare compliance certificates at the time of order.
Drawing requirements: Supply revision-controlled drawings identifying functional datums, realistic tolerances for a compliant plastic, surface finishes, and critical inspection points.
Quality plan: Agree on first-article inspection (FAI) requirements, measurement methods (e.g., CMM with low touch-force), and reporting formats.
Manufacturing validation: Ask the supplier to confirm that your tolerances are feasible for CNC-machined PP, or if injection molding is required to achieve the desired feature set.
Purchasing rule:Verbal descriptions such as “standard PP” or “any polypropylene” are insufficient for industrial parts. Always tie the PO to a specific grade and revision-controlled drawing.
Common applications include packaging and closures, reusable containers, automotive trim, pipe and fitting systems, chemical-handling components, fibers, consumer products, and laboratory supplies.
Yes, PP is highly resistant to many aqueous acids, alkalis, and process fluids. However, compatibility depends on the exact chemical mixture, concentration, and temperature. It is not suitable for strong oxidizers or certain halogenated hydrocarbons.
Yes. PP stock can be milled or turned for custom parts, prototypes, and low-volume components. Because it is compliant, generates stringy chips, and expands with heat, careful workholding and sharp tooling are required.
PP homopolymer is stiffer and stronger at room temperature but becomes brittle near 0°C. PP copolymers (random or block) offer better impact resistance, especially in cold environments, and varying degrees of clarity.
Due to its extremely low surface energy, standard adhesives will not stick to PP. To bond it, the surface must be treated (corona, plasma, or flame treatment), a specialized polyolefin primer must be used, or the parts must be thermally welded (e.g., hot gas or ultrasonic welding).
Use current supplier documents and applicable legal texts for material approval. The sources below support the general overview discussed in this article.
ExxonMobil Product Solutions — Polypropylene Technical Data Sheets.
SABIC — Polypropylene (PP) product portfolio.
U.S. Electronic Code of Federal Regulations, 21 CFR § 177.1520 — Olefin polymers. (Food contact regulations).
Ready to transform your CAD file into a custom part? Upload your design to get a free, precise quote.
Get Your Instant Quote