1. Basic Material Information
Standard Material Designations & Classification
Item | PVC |
Chemical name | Polyvinyl Chloride |
Common abbreviation | PVC |
Rigid form | PVC-U / UPVC |
Plasticized form | PVC-P |
Chlorinated form | CPVC |
Material category | Thermoplastic |
Polymer type | Amorphous thermoplastic |
Common CNC stock | Sheet, plate, rod, tube, block |
Typical appearance | White, gray, black, clear/specialty colors |
Common manufacturing processes | CNC machining, extrusion, injection molding |
Relevant standards | ISO 1163; ASTM D1784 |
Typical applications | Chemical equipment, piping, electrical, industrial machinery |
PVC does not use a universal metallic-style UNS designation.
For purchasing, the specification should identify:
PVC type
Grade
Color
Chemical environment
Temperature requirements
Flame requirements
Electrical requirements
Applicable certification
PVC Material Family
The PVC family can be broadly divided into three core types, with distinct performance and application scenarios:
PVC-U — Rigid PVC This is the most relevant form for CNC machining. Typical properties include high chemical resistance, good stiffness, excellent electrical insulation, ultra-low moisture absorption and superior machinability, which makes it the mainstream material for industrial custom CNC parts.
PVC-P — Plasticized PVC Plasticizers make PVC softer and more flexible. It is commonly used for flexible tubing, cable insulation, seals and flexible sheets. Its machining performance and mechanical properties are vastly different from rigid PVC, rarely used for precision CNC structural parts.
CPVC — Chlorinated PVC CPVC has increased chlorine content and generally provides better temperature resistance than standard PVC, suitable for high-temperature chemical industrial scenarios that ordinary PVC cannot adapt to.
Core Material Positioning
Rigid PVC is positioned as a cost-effective industrial thermoplastic, especially suitable for scenarios where chemical resistance and electrical insulation are prioritized over high mechanical strength or high-temperature performance.
Its major advantages include:
Excellent chemical and corrosion resistance
Ultra-low water absorption
Stable electrical insulation performance
Simple and efficient CNC machining
Low material and processing cost
Low density, lightweight structure
2. PVC Physical Properties
Property | Typical PVC-U Range |
Density | ~1.35–1.45 g/cm³ |
Tensile strength | ~40–60 MPa |
Tensile modulus | ~2.5–3.5 GPa |
Elongation at break | ~20–80% |
Flexural modulus | ~2.5–3.5 GPa |
Hardness | Typically Rockwell R100–R125 |
Water absorption | Typically <0> |
Thermal conductivity | ~0.15–0.20 W/m·K |
Glass transition temperature | ~75–85°C |
Recommended continuous service temperature | Commonly ~50–60°C |
Short-term temperature capability | Higher, depending on grade |
Density
Rigid PVC typically has a density around 1.35–1.45 g/cm³. Although denser than many common engineering plastics, PVC is still considerably lighter than steel. It balances moderate weight, good structural stiffness, low cost and excellent chemical resistance, becoming the preferred material for cost-effective industrial structural accessories.
Tensile Strength & Stiffness
Rigid PVC generally provides tensile strength around 40–60 MPa and modulus around 2.5–3.5 GPa, with sufficient stiffness for manufacturing protective covers, fixtures, housings, fluid-handling components and electrical insulating parts. However, it is not suitable for high-load structural components, where PEEK, POM, nylon and other reinforced polymers perform better.
Impact Resistance
Rigid PVC has moderate impact resistance, which is greatly affected by temperature, wall thickness, material grade, stress concentration and additives. PVC will become significantly brittle at low temperatures. For scenarios with repeated impact or severe mechanical shock, impact-resistant PC or modified engineering plastics are more recommended.
Thermal Performance
Standard rigid PVC has a low glass transition temperature of 75–85°C, with a continuous service temperature limited to 50–60°C, which is the core limitation of PVC materials. For high-temperature chemical working environments, CPVC or other high-performance engineering plastics should be selected instead.
Dimensional Stability
PVC features extremely low moisture absorption, effectively avoiding dimensional changes caused by humidity, with better stability than hygroscopic materials such as nylon. However, its high thermal expansion coefficient will cause slight dimensional deviation with temperature changes, which needs to be considered in precision part processing.
Wear Resistance
Standard PVC only has moderate wear resistance, so it is not suitable for high-speed bearings, precision gears, high-load sliding surfaces and severe abrasion scenarios. POM, nylon, UHMW-PE and other tribological plastics are better alternatives for wear-resistant parts.
3. PVC Chemical Properties
Chemical Composition
PVC is a polymer based on vinyl chloride repeating units, composed of carbon, hydrogen and chlorine elements. Commercial PVC products are added with thermal stabilizers, impact modifiers, lubricants, pigments, plasticizers and processing aids, and different formulations directly determine the material's final performance.
Chemical Resistance
Chemical resistance is the core advantage of rigid PVC. It has excellent tolerance to most dilute acids, alkalis, salts, aqueous solutions and inorganic chemicals, making it widely used in corrosive chemical processing environments.
Nevertheless, PVC is sensitive to partial organic solvents. Ketones, aromatic hydrocarbons, individual chlorinated solvents and esters may cause swelling, softening and material degradation. Chemical compatibility must be verified according to actual concentration and working temperature.
Corrosion Resistance
Different from metal materials, PVC will not produce electrochemical corrosion. It can stably resist erosion from acids, alkalis, salt solutions, chemical fumes and humid environments, and is an ideal lightweight alternative to metal for chemical industrial equipment.
Water Resistance
PVC has ultra-low water absorption (less than 0.1%), ensuring stable dimensional performance in long-term humid and water-contact environments, without deformation or performance attenuation caused by moisture absorption, which is far superior to nylon materials.
UV Resistance
Standard ordinary PVC is prone to aging and degradation under long-term UV exposure, resulting in discoloration, surface chalking, reduced impact resistance and material embrittlement. Outdoor working parts must adopt professional UV-stabilized PVC grades.
Flame Behavior
Due to the chlorine-containing molecular structure, PVC has natural flame-retardant properties, better than most hydrocarbon plastics. It should be noted that the flame-retardant level is grade-specific, and the actual fire protection certification must be confirmed according to the material model, instead of generalizing all PVC materials.
Thermal Decomposition
A key processing taboo for PVC is thermal decomposition. Overheating during CNC machining will cause the material to release hydrogen chloride (HCl) gas. Therefore, it is necessary to use sharp tools, optimize cutting parameters and strengthen chip evacuation to avoid heat accumulation.
Welding & Bonding
PVC has excellent bonding and assembly performance, supporting solvent cement bonding, adhesive bonding, thermal welding and mechanical fastening. Solvent welding is the most common process for PVC pipe and fitting connection. It is necessary to verify the compatibility between the adhesive/solvent and the PVC formulation before construction.
4. PVC CNC Machinability Analysis
Machining Difficulty: Easy–Moderate
Rigid PVC is one of the easiest industrial plastics for CNC processing, supporting CNC milling, turning, drilling, tapping, routing, sawing and engraving. The core processing difficulty is not cutting resistance, but precise heat control to avoid material thermal damage.
Recommended Cutting Tools
Tool sharpness is the key to high-quality PVC machining. Recommended tooling includes sharp carbide end mills, polished carbide cutters, single-flute/double-flute special plastic cutters and precision sharp drills. Sharp cutting edges can effectively reduce heat generation, tool rubbing, burrs and surface scratches.
General CNC Cutting Parameter Guidance
The following parameters are reliable starting ranges for rigid PVC machining, which can be adjusted according to tool size, spindle performance, material grade, part thickness and surface finish requirements.
Parameter | Typical Starting Range |
Cutting speed | ~150–500 m/min |
Feed per tooth | ~0.05–0.25 mm/tooth |
Tool | Sharp carbide |
Coolant | Air blast / compatible coolant |
Chip evacuation | High priority |
Finishing | Light finishing pass |
CNC Milling PVC
Rigid PVC is highly suitable for CNC milling processes, including pocketing, profiling, slotting, drilling, contouring, engraving and threading. It is the best choice for low-volume, customized large-scale industrial parts that are not suitable for injection molding production, with high processing efficiency and low cost.
CNC Turning PVC
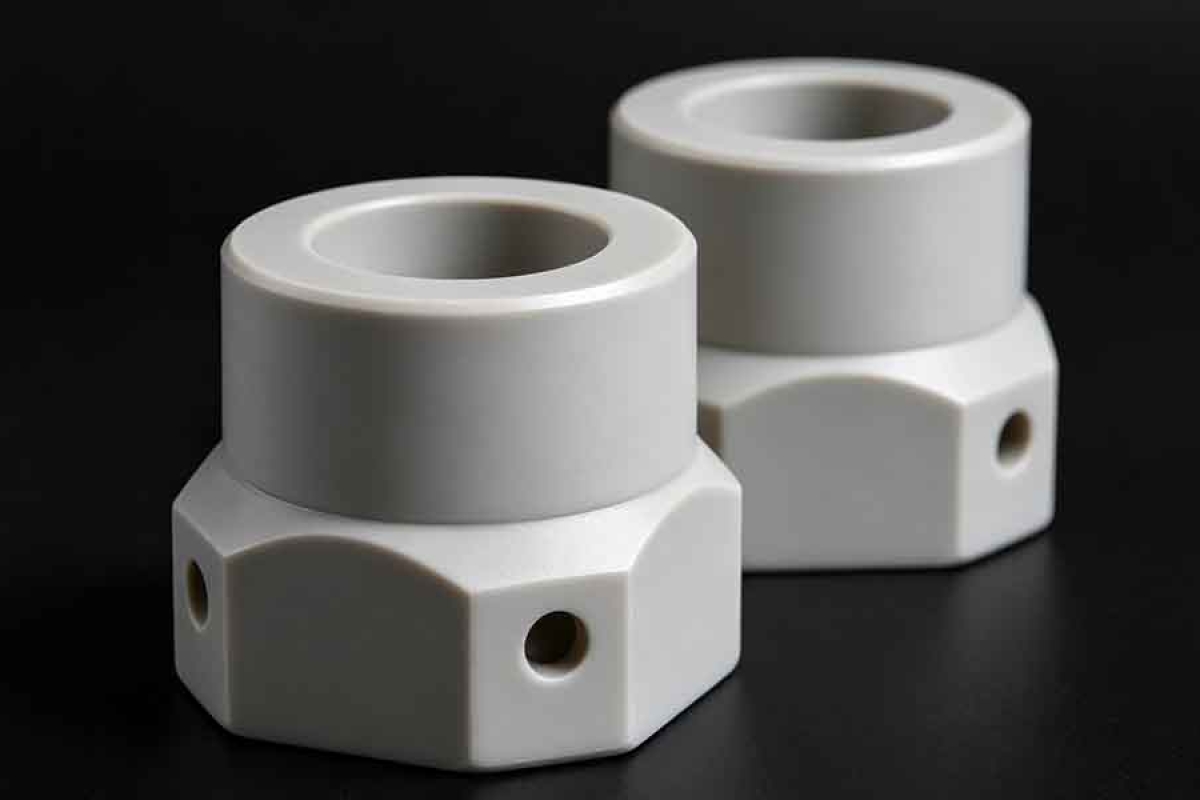
CNC turning can process PVC into various cylindrical parts such as bushings, rings, sleeves, spacers, pipe fittings, valve components and cylindrical housings. Adopting sharp tools and low cutting force can effectively prevent material deformation and ensure dimensional accuracy of rotary parts.
Drilling PVC
PVC drilling has low processing difficulty, but improper operation will cause burrs, heat accumulation, hole distortion and material melting. Stable feed rate and smooth chip evacuation are essential to ensure neat hole wall and high precision.
Tapping PVC
PVC can be directly tapped for low and medium-load threaded connection scenarios. Due to its lower mechanical strength than POM and nylon, high-load threaded structures need to adopt lengthened engagement, threaded inserts or metal embedded parts to improve connection durability.
Common PVC CNC Machining Problems
1. Melting / Thermal Damage Causes: Excessive spindle speed, dull tools, too low feed rate, poor chip evacuation and tool rubbing. Solutions: Replace sharp cutters, optimize speed and feed parameters, match air blast cooling, and ensure smooth chip removal to avoid heat accumulation.
2. Burr Formation Burrs are easy to appear at hole exits, slots, thin edges and intersecting features. Using ultra-sharp tools and independent light finishing passes can greatly reduce burrs and reduce post-processing workload.
3. Edge Chipping Rigid PVC will become brittle at low temperature, prone to edge chipping during cutting. Optimize cutting tools, reduce instantaneous cutting force, increase material support and avoid sudden tool engagement to solve the problem.
4. Thin-Wall Deformation Thin-walled PVC parts are easy to deform under rigid clamping force. Soft jaws, vacuum fixtures, dispersed clamping and reduced pressure can effectively protect thin-wall structures.
5. Surface Scratches PVC surfaces are easy to be scratched by fixtures, chips and manual handling. Retaining protective film, keeping the processing environment clean and adopting independent protective packaging can ensure the cosmetic quality of parts.
CNC Tolerance Capability
With standardized process control, rigid PVC CNC machining can stably achieve ±0.05 mm precision for conventional features. For most industrial PVC parts, overly tight tolerances are unnecessary and will increase processing costs. Precision standards can be reasonably formulated according to actual functional requirements.
Surface Finish
Under matched tooling and finishing processes, CNC-machined rigid PVC can reach Ra 1.6–3.2 μm surface finish. Optimized processing parameters can achieve finer smoothness, meeting the functional and cosmetic needs of most industrial parts.
5. Typical PVC Applications & Part Scenarios
Chemical Processing Equipment
This is the core application scenario of rigid PVC. CNC-machined PVC valve components, flanges, pump parts, pipe fittings, chemical tanks, protective covers and mounting plates can resist the erosion of various corrosive media, which is irreplaceable for metal parts in chemical environments.
Water & Fluid Handling
PVC fluid manifolds, pipe fittings, valve bodies, flanges, pump components and pipe supports rely on ultra-low water absorption and corrosion resistance to avoid rust and mildew, and are widely used in water treatment and industrial fluid delivery systems.
Industrial Automation
PVC is used to manufacture automation equipment protective covers, safety guards, tooling fixtures, mounting plates, cable routing parts and machine enclosures. It is cost-effective and insulating, but not suitable for high-temperature automation working environments.
Electrical & Electronics
With excellent insulation performance, PVC is widely used for electrical insulating spacers, protective covers, mounting components, cable management parts and insulating housings. Flame-retardant grades can be selected to meet electrical safety certification requirements.
Laboratory Equipment
Chemical-resistant PVC fixtures, laboratory functional components, fluid-handling parts and protective covers can adapt to the complex chemical environment of laboratories, with stable performance and low maintenance cost.
Semiconductor & Chemical Equipment
Modified high-purity PVC can be used for semiconductor and chemical equipment fixtures, exhaust components, protective covers and fluid manifolds. It needs to meet strict standards of low outgassing, low particle generation and chemical compatibility.
6. Our PVC CNC Machining Advantages
Professional PVC Grade Selection
Evefab's professional engineering team provides targeted material selection services, accurately distinguishing PVC-U, PVC-P, CPVC and modified rigid PVC grades. We match the most suitable material according to the working environment such as chemical corrosion, temperature, mechanical load, UV exposure and electrical flame-retardant requirements, avoiding material mismatch failure.
Experienced CNC Machining Process
Evefab has mature standardized PVC CNC processing technology, strictly controlling core processing links such as cutting heat, tool sharpness, chip evacuation, clamping force, burr removal and surface protection. We adjust processing parameters according to different PVC formulations and part structures to ensure stable part quality.
Precision CNC Manufacturing
We support high-precision customization of PVC parts, accurately controlling core indicators such as hole diameter, flatness, parallelism, position accuracy, concentricity, profile and thread size. All parts can be produced and inspected in strict accordance with GD&T geometric tolerance standards to meet precision industrial assembly requirements.
Custom Chemical-Equipment Components
Focusing on chemical industry application scenarios, Evefab customizes various PVC corrosion-resistant parts including flanges, valve components, fluid manifolds, pipe fittings, protective covers and pump accessories. We verify material chemical compatibility for customers to ensure long-term stable operation of equipment parts.
Prototype to Batch Production
Evefab supports full-cycle production services of PVC parts, including one-off custom parts, equipment replacement parts, engineering prototypes, small-batch trial production and mass batch production. Optimized fixtures and tool paths effectively improve production efficiency and reduce unit cost for large orders.
Quality Inspection & Material Documentation
We implement strict full-process quality control, including dimensional inspection, GD&T verification, thread detection, surface finish testing and visual cosmetic inspection. Complete material certification and quality inspection reports can be provided to meet industrial compliance requirements.
PVC CNC Machining Material Selection Summary
Requirement | PVC-U Suitability |
CNC milling | Excellent |
CNC turning | Excellent |
Drilling | Excellent |
Tapping | Good |
Chemical resistance | Excellent |
Water resistance | Excellent |
Electrical insulation | Excellent |
Wear resistance | Moderate |
Impact resistance | Moderate |
Dimensional stability | Good |
Moisture absorption | Very low |
High-temperature capability | Limited |
Outdoor UV resistance | Grade-dependent |
Thin-wall machining | Good |
Chemical equipment | Excellent |
Pipe/valve components | Excellent |
High-load mechanical parts | Limited |
Cost efficiency | Excellent |
PVC vs. POM vs. PP vs. PE vs. CPVC
Property | PVC-U | POM | PP | PE | CPVC |
Chemical resistance | Excellent | Good | Excellent | Excellent | Excellent |
Machinability | Excellent | Excellent | Moderate | Moderate | Excellent |
Dimensional stability | Good | Excellent | Moderate | Moderate | Good |
Stiffness | Good | Excellent | Moderate | Low–Moderate | Good |
Wear resistance | Moderate | Excellent | Good | Good | Moderate |
Temperature capability | Limited | Good | Good | Limited | Better than PVC |
Water absorption | Very low | Very low | Very low | Very low | Very low |
Electrical insulation | Excellent | Excellent | Excellent | Excellent | Excellent |
Chemical equipment | Excellent | Moderate | Excellent | Excellent | Excellent |
Precision mechanical parts | Good | Excellent | Moderate | Limited | Good |
Cost | Low | Moderate | Low | Low | Moderate |
Final Engineering Recommendation
PVC is one of the most practical and cost-effective CNC machining materials for industrial customized parts. It performs excellently in scenarios requiring chemical corrosion resistance, electrical insulation and low moisture absorption, and is widely used in chemical processing equipment, fluid-handling components, laboratory fixtures, protective covers and electrical insulating parts.
The biggest limitation of standard PVC-U is its poor high-temperature resistance, so it is not suitable for long-term high-temperature working environments. For high-temperature corrosive scenarios, CPVC, PP, PVDF or PEEK materials can be selected according to actual working conditions.
For precision PVC CNC parts, engineers should specify the exact material grade, working temperature, chemical environment, dimensional tolerance and certification standards instead of simply marking "PVC".
Contact Evefab for professional CNC machining quotes and DFM design consultation for custom PVC components. We provide one-stop services including PVC-U/CPVC material selection, corrosion-resistant part customization, precision tolerance control, surface finishing and batch production planning to meet your diverse industrial processing needs.
Get an Instant Quotefor your custom PVC parts today.