Produkcja na żądanie dostawców CNC, stabilna dostawa i spójna jakość.Natychmiastowa cytacja
Gotowy na testowanie swojego projektu? Prześlij swoje części do bezpłatnej analizy DFM.
Uzyskaj natychmiastową ofertęRodzaj materiału
Nazwa materiału
Kompatybilność procesu

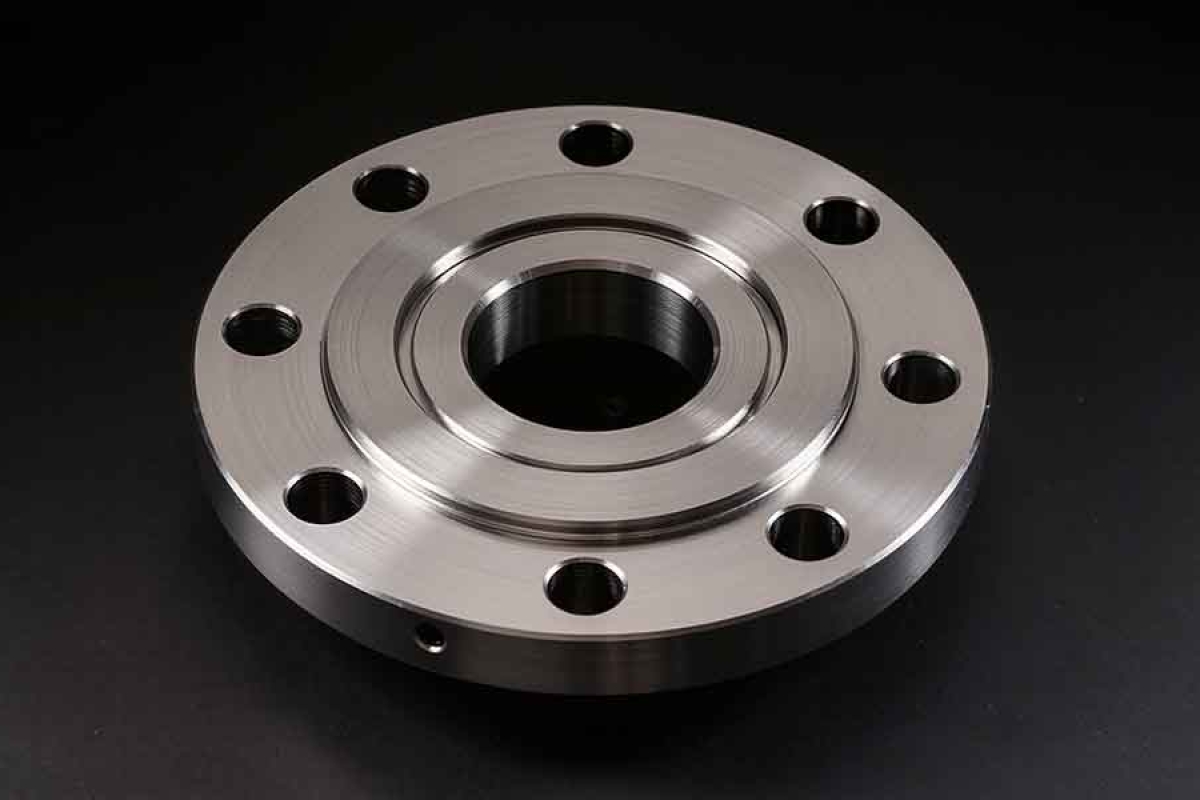
Stal nierdzewna 416jest wolno obróbkową martenzytową stalą nierdzewną zawierającą kontrolowane dodatki siarki w celu poprawy obróbkowości. Jest szeroko stosowany doprecyzyjna obróbka CNC, automatyczna obróbka śrub, wały, zawory, przekładnia, komponenty pompy, elementy mocujące i inne części obróbane o dużej objętościgdzie wydajność obróbki jest ważniejsza niż maksymalna odporność na korozję.
Stal nierdzewna 416 jestmartensityczna stal nierdzewna chromowaPochodzi z rodziny 410. Jego definiującą cechą jest umyślne dodanie siarki, co poprawia efektywność łamania szlifów i obróbki.
Nieruchomość | Informacje |
|---|---|
Materiał | Stal nierdzewna 416 |
AISI / SAE | 416 |
UNS | S41600 |
Oznaczenie EN | X12CrS13 |
Materiał nr. | 1.4005 |
JIS | SUS 416 |
BS | 416S21 |
AFNOR | Z11CF13 |
Rodzina ze stali nierdzewnej | Martenzytowa stal nierdzewna |
Chrom | ~12–14% |
Główny element specjalny | siarka |
Magnetyczny | Tak |
Podstawowa zaleta produkcyjna | Doskonała przetwarzalność |
Równoważność międzyAISI 416, UNS S41600, EN 1.4005 i X12CrS13jest obsługiwany przez wielu dostawców materiałów i arkusze techniczne.
Stainless Steel 416 is best positioned as a precision-machining stainless steel, rather than as a general-purpose corrosion-resistant stainless steel.
Its sulfur addition makes it particularly suitable for:
Toczenie CNC
Swiss-type CNC machining
Automatic screw machining
High-volume precision components
Complex turned parts
Shafts and pins
Komponenty zaworu
Mocowniki
Swiss Steel specifically describes 1.4005 as 1.4006 with controlled sulfur addition to improve machinability and automated machining capability. However, the same sulfur addition reduces corrosion resistance and surface-finish quality compared with 1.4006.
The following values are representative engineering values. Actual mechanical properties depend on the heat-treatment condition, product form, diameter/thickness and governing specification.
Nieruchomość | Typical Value |
|---|---|
Gęstość | ~7.70–7.80 g/cm³ |
Elastic modulus | ~200–215 GPa |
Poisson's ratio | ~0.27–0.30 |
Przewodność cieplna | ~24.9 W/m·K at 100°C |
Specific heat | ~460 J/kg·K |
Thermal expansion, 20–100°C | ~10.5 × 10⁻⁶/K |
Thermal expansion, 20–200°C | ~11.0 × 10⁻⁶/K |
Thermal expansion, 20–300°C | ~11.5 × 10⁻⁶/K |
Thermal expansion, 20–400°C | ~12.0 × 10⁻⁶/K |
Melting range | ~1,480°C class |
Swiss Steel reports a density of approximately 7.70 kg/dm³, elastic modulus around 215 GPa, thermal conductivity around 30 W/m·K at 20°C and a thermal expansion coefficient of 10.5–12.0 × 10⁻⁶/K over 20–400°C. Other commercial datasheets report approximately 24.9 W/m·K at 100°C.
Mechanical properties must always be tied to the material condition. 416 does not have one universal tensile strength because annealed and quenched-and-tempered conditions behave very differently.
For annealed material, representative values include:
Nieruchomość | Typical Value |
|---|---|
Wytrzymałość na rozciąganie | up to ~730 MPa |
Twardość | ≤ ~220 HB |
Siła wydajności | Condition-dependent |
Elongation | Condition-dependent |
For quenched-and-tempered conditions, representative values can reach approximately:
Yield strength: ~450 MPa or higher
Tensile strength: ~650–850 MPa
Elongation: ~10–12%
depending on product size and heat-treatment condition.
416 can be hardened by heat treatment. Typical processing involves:
Austenitizing → quenching → tempering
Technical datasheets commonly specify hardening temperatures around 950–1,000°C, followed by air or oil quenching depending on the product and process.
This provides an important advantage when a CNC part needs both:
excellent machinability during manufacturing + higher hardness after heat treatment.
The EN 1.4005 / X12CrS13 composition is approximately:
Element | Typical EN Range / Limit |
|---|---|
Carbon (C) | 0.06–0.15% |
Chromium (Cr) | 12.0–14.0% |
Sulfur (S) | 0.15–0.35% |
Silicon (Si) | ≤1.00% |
Manganese (Mn) | ≤1.50% |
Phosphorus (P) | ≤0.040% |
Molybdenum (Mo) | ≤0.60% |
Iron (Fe) | Balance |
These ranges are consistent with EN 10088 material references for 1.4005.
This is the defining characteristic of 416.
Sulfur promotes the formation of manganese sulfide inclusions, which help:
Break chips
Reduce continuous chip formation
Improve tool productivity
Reduce cutting forces in suitable operations
Improve automatic machining performance
This is why 416 is frequently selected for CNC turning and automatic screw-machine applications.
However, the same sulfide inclusions can negatively affect:
Odporność na korozję
Surface quality
Polerowanie
Spawalność
This is the fundamental engineering trade-off of 416.
Although 416 contains approximately 12–14% chromium, it should not be treated as equivalent to 304 or 316 stainless steel in corrosion resistance.
The sulfur addition reduces resistance to localized corrosion, particularly:
Pitting
Crevice corrosion
Chloride-containing environments
Aggressive chemical environments
Swiss Steel specifically warns that 1.4005 has relatively poor corrosion resistance compared with other stainless grades and that the sulfur addition increases susceptibility to pitting and crevice corrosion.
416 is more appropriate for:
Indoor machinery
Mild atmospheric environments
Dry mechanical systems
Automotive components
Zawory
Shafts
Mocowniki
Precision mechanisms
It is generally not the first choice for:
Marine environments
Saltwater exposure
Chloride-rich chemical processing
High-corrosion outdoor environments
For those applications, engineers may consider 304, 316/316L or other corrosion-resistant grades, depending on the actual environment.
Weldability: Poor to limited.
416 combines:
Martensitic metallurgy
Relatively high carbon
Sulfur additions
which makes welding considerably less attractive than welding austenitic stainless steels such as 304L or 316L.
Some technical sources recommend avoiding welding where possible because of hardening and cracking risks.
For a welded design, the material should therefore be reviewed specifically for the welding procedure, preheating, filler selection and post-weld heat treatment requirements.
Yes. 416 is one of the most machinable stainless steel grades.
Its primary commercial advantage is exactly this characteristic.
Machining difficulty: Easy
Compared with:
304 stainless steel
316 stainless steel
17-4 PH stainless steel
Titanium alloys
Inconel alloys
416 can provide significantly better chip control and machining productivity under suitable conditions.
Technical machining databases list 416 as a free-machining stainless grade and provide relatively high cutting-speed ranges compared with many other stainless steels.
For precision CNC machining, recommended tooling commonly includes:
Coated carbide inserts
PVD-coated carbide turning tools
Carbide end mills
Carbide drills
Carbide reamers
Sharp carbide threading tools
Tool selection should account for whether the material is:
Wygrzane
Hardened
Quenched and tempered
Hardened 416 requires different tooling and cutting conditions from annealed material.
For stable turning conditions, published machining data gives representative cutting-speed ranges around:
370–505 m/min
For stable milling with short tool overhang and rigid clamping:
235–315 m/min
Machining data also gives approximate ranges of:
Parting: 150–200 m/min
Grooving: 225–300 m/min
Drilling: 180–245 m/min
These should be regarded as starting values, not universal production settings. Tool grade, insert geometry, workholding, machine rigidity, diameter, depth of cut and coolant strategy must be considered when establishing actual production parameters.
The same sulfide inclusions that improve machinability can affect surface appearance and polishability.
Therefore, 416 is excellent for:
machined functional surfaces
but less suitable when the component requires:
mirror polishing or highly decorative surfaces.
Swiss Steel specifically identifies polishing as unfavorable for 1.4005.
416 is highly machinable, but tool life can still be affected by:
Excessive cutting speed
Poor insert geometry
Insufficient coolant
Excessive depth of cut
Interrupted cutting
Hardened material
For production, tool-life monitoring is particularly important when running automated turning operations.
If the component is machined before hardening, subsequent heat treatment can introduce dimensional changes.
For tight-tolerance parts, a process such as:
Rough machining → heat treatment → semi-finishing → finishing → inspection
may be preferable to completing all critical dimensions before hardening.
For long shafts and slender turned components, chatter can still occur despite the material's excellent machinability.
Solutions include:
Shorten tool overhang.
Improve workholding rigidity.
Use appropriate insert geometry.
Optimize feed and cutting speed.
Support long shafts with a tailstock or steady rest.
Use optimized roughing/finishing passes.
416 can achieve tight dimensional tolerances through properly controlled CNC processes.
A practical precision CNC capability may be approximately:
±0.01–0.05 mm
depending on:
Part size
Geometry
Machine capability
Heat-treatment condition
Narzędzia
Workholding
Inspection method
For critical dimensions, tighter tolerances may require specialized process control, grinding or other secondary operations.
Typical machined surface roughness can be approximately:
Ra 0.8–3.2 µm
depending on the tool, machining strategy and surface requirements.
However, engineers should distinguish between machining roughnessipolishability. 416's sulfur content makes it less suitable when a very high cosmetic polish is required.
416 is highly compatible with:
Toczenie CNC
Swiss CNC machining
Automatic screw machining
frezowanie 3-osi
4-axis machining
5-axis machining
Drilling
Boring
Reaming
Threading
Thread milling
Szlifowanie
416 is particularly attractive for Swiss-type CNC machining.
Its free-machining characteristics make it suitable for:
Small shafts
Szpilki
Bushings
Screws
Komponenty zaworu
Złącza
Precision turned parts
This is one of the strongest manufacturing use cases for the material.
416 is particularly well suited to high-volume automatic machining, where chip control and cycle-time efficiency have a significant impact on production economics.
4
Typical components include:
Shafts
Komponenty zaworu
Mocowniki
Gears
Szpilki
Precision turned parts
416 is attractive where high machining productivity and moderate corrosion resistance are required.
Typical components include:
Pump shafts
Valve stems
Komponenty zaworu
Bushings
Rotating components
The combination of machinability and heat-treatable hardness makes 416 useful for these applications.
However, the fluid chemistry must be evaluated carefully because its corrosion resistance is substantially lower than 316/316L.
Typical parts include:
Precision shafts
Gears
Szpilki
Bushings
Mocowniki
Motor components
Mechanical transmission components
416 is particularly attractive when the part will be produced in significant quantities through CNC turning.
This is one of the material's strongest applications.
Examples include:
Screws
Nuts
Studs
Szpilki
Threaded components
Small turned components
The controlled sulfur content helps improve chip breaking and automated machining efficiency.
416 can also be used for:
Solenoid components
Motor shafts
Mechanical actuator components
Precision mechanical housings
Electromechanical parts
It is magnetic, which can be an advantage or disadvantage depending on the design.
DlaStainless Steel 416 CNC machining, process control should focus on maintaining the balance between machining productivity, dimensional accuracy, heat treatment and corrosion requirements.
We can support 416 projects with:
AISI 416 / UNS S41600 material sourcing
EN 1.4005 / X12CrS13 material options
Material selection support
Material Test Reports (MTR)
Heat/lot traceability
Incoming material verification
Required material documentation
For international projects, the required specification should be established before production to prevent substitution between nominally equivalent grades with different product requirements.
Our manufacturing process can support:
Toczenie CNC
Swiss-type CNC machining
Frezowanie CNC
4-axis machining
5-axis machining
Automatic screw machining
Prototype production
Small-batch production
Medium-volume production
For high-volume turned components, 416 can provide a strong combination of machinability, cycle-time efficiency and dimensional repeatability.
Where higher hardness or strength is required, 416 can be supplied or processed through suitable:
Utwardzanie
Tłuszczenie
hartowanie
Stress-relief treatments
Heat treatment should be incorporated into the dimensional-control strategy because it can affect final part geometry.
Depending on project requirements, inspection can include:
CMM inspection
Micrometer measurement
Bore gauges
Thread gauges
Height gauges
Hardness testing
Surface roughness inspection
Inspekcja artykułu pierwszego (FAI)
Material Test Reports (MTR)
Critical dimensions can be controlled according to the customer's GD&T drawing and inspection requirements.
Possible post-processing options depend on the application and required appearance, including:
Passivation where appropriate
Szlifowanie
Szczotkowanie
Blasting
Controlled polishing where suitable
However, 416 should not be selected primarily for decorative mirror finishing. Its sulfur content makes highly polished surfaces more difficult than with suitable low-sulfur stainless grades.
Requirement | 416 Assessment |
|---|---|
CNC machinability | Doskonałe |
Obróbka szwajcarska | Doskonałe |
Automatic screw machining | Doskonałe |
Strength | Good–High after heat treatment |
Hardness potential | Dobrze. |
Odporność na korozję | Moderate to Low |
Odporność na zużycie | Good after suitable heat treatment |
Spawalność | Biedni |
Polishability | Poor to Moderate |
Magnetyczny | Tak |
High-volume production | Doskonałe |
Precision turning | Doskonałe |
5-axis machining | Dobrze. |
Marine/chloride environments | Generally unsuitable |
Nieruchomość | 416 | 410 | 304 |
|---|---|---|---|
Obróbalność | Doskonałe | Dobrze. | Umiarkowany |
Odporność na korozję | Moderate–Low | Umiarkowany | Wysoki |
Obróbka cieplna | Tak | Tak | Nie |
Magnetyczny | Tak | Tak | Generally non-magnetic when annealed |
Spawalność | Biedni | Limited | Doskonałe |
Automatic machining | Doskonałe | Dobrze. | Umiarkowany |
High-volume turned parts | Doskonałe | Dobrze. | Umiarkowany |
Decorative polishing | Biedni | Umiarkowany | Doskonałe |
The key selection principle is simple:
Choose 416 when machining productivity and dimensional manufacturing efficiency are priorities; choose 304/316-family grades when corrosion resistance is the dominant requirement.
DlaStainless Steel 416 / 1.4005 / X12CrS13 CNC machining, the material's greatest advantage is its free-machining behavior. It is particularly well suited to precision turned parts, shafts, valve components, gears, fasteners and automated high-volume production.
Evefab can support the complete manufacturing workflow from DFM review and material selection through CNC machining, heat treatment, dimensional inspection, MTR documentation and production delivery.
View the Evefab Stainless Steel 416 CNC Machining page
Contact Evefab to request a Stainless Steel 416 CNC machining quote and DFM review for prototypes, small-batch production or medium-volume manufacturing.
Uzyskaj natychmiastową ofertędla niestandardowych części ze stali nierdzewnej 416 dzisiaj.
Gotowy do przekształcenia pliku CAD w niestandardową część? Prześlij swój projekt, aby uzyskać bezpłatną, precyzyjną ofertę.
Uzyskaj natychmiastową ofertę