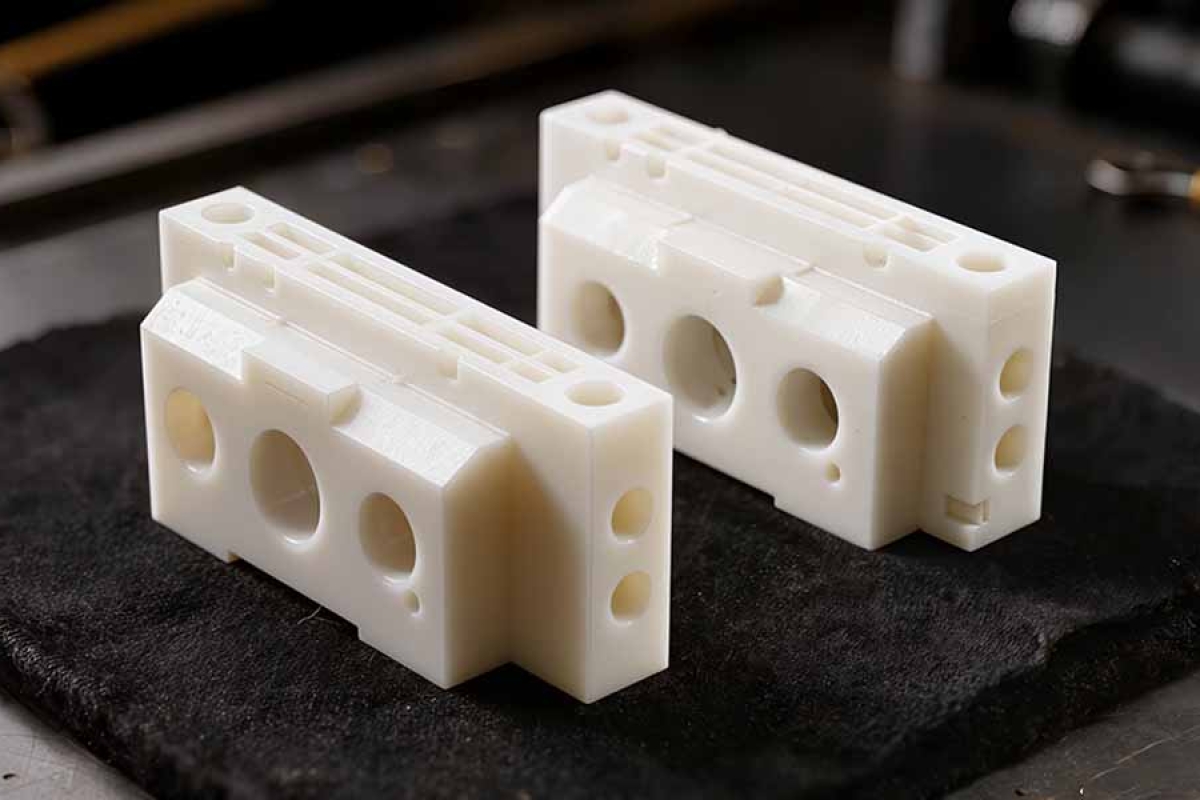
Was ist POM Material?
POM (Polyoxymethylen), allgemein als Acetal bekannt, ist ein leistungsstarker technischer Thermoplast, der weit verbreitet wird für PräzisionsCNC-bearbeitete Teile. Delrin® ist eine bekannte kommerzielle Marke von Acetalhomopolymeren, während POM auch Copolymergraden anderer Hersteller umfasst. Das Material verbindet geringe Reibung, gute Verschleißbeständigkeit, Dimensionsstabilität, Steifigkeit und ausgezeichnete Bearbeitbarkeit, was es besonders wertvoll für Zahnräder, Buchsen, Rollen, Präzisionsarmaturen, Führungskomponenten und mechanische Teile macht.
Hinweis zur Materialterminologie: „POM“ und „Delrin“ sollten nicht automatisch als identische Spezifikationen behandelt werden. POM ist die Polymerfamilie; Delrin® ist ein eingetragener Handelsname, der Acetalhomopolymerprodukten zugeordnet ist. Die tatsächlichen Eigenschaften hängen von der spezifischen Klasse und dem Lieferantendatenblatt ab.
1. Grundmaterialinformationen
Materialbezeichnung & Klassifizierung
Artikel | POM / Acetal |
Standard Material Name | Polyoxymethylen |
Allgemeine Namen | POM, Acetal, Polyacetal |
Handelsname | Delrin® für spezifische Produktqualitäten von DuPont/Celanese |
Materialkategorie | Technische Thermoplastik |
Polymerstruktur | Halbkristalline thermoplastische |
Allgemeine Formulare | Blech, Platte, Stange, Rohr, Billet |
Gemeinsame Herstellungsmethoden | CNC-Bearbeitung, Spritzgießen, Extrusion |
ISO-Materialfamilie | POM |
Relevante Normen | ISO 9988; ASTM D4181 und andere anwendungs-/testspezifische Normen |
POM is generally divided into two major material families:
POM-H (homopolymer acetal) — typically higher stiffness, strength and dimensional stability.
POM-C (copolymer acetal) — generally offers improved resistance to thermal and chemical degradation and is widely used for engineering components.
The actual grade should be specified according to the supplier's datasheet because additives, reinforcement and formulation can substantially change performance.
Core Positioning
POM is one of the most important engineering plastics for precision mechanical components.
Compared with ABS, POM generally offers:
Better wear resistance
Lower friction
Higher stiffness
Better dimensional stability
Better machinability for precision mechanical components
Compared with PEEK, POM generally offers:
Lower cost
Easier machining
Lower temperature capability
Lower chemical and mechanical performance at elevated temperatures
This makes POM particularly attractive for precision CNC plastic parts where mechanical movement and dimensional accuracy are important.
2. POM Physical Properties
The following values represent typical ranges for unfilled commercial POM grades. They are not universal specification limits. Homopolymer and copolymer grades can differ significantly.
Immobilien | Typical POM Range |
Dichte | ~1.40–1.43 g/cm³ |
Zugfestigkeit | ~60–75 MPa |
Zugmodul | ~2.5–3.5 GPa |
Verlängerung beim Bruch | ~10–40% |
Biegemodul | ~2.5–3.5 GPa |
Härte | Typically Rockwell M80–M95 |
Water absorption | Generally <0> |
Wärmeleitfähigkeit | ~0.3 W/m·K |
Melting temperature | ~160–180°C |
Glass transition temperature | Approximately −60°C |
Continuous service temperature | Commonly around 90–105°C |
Coefficient of friction | Low; grade and counterface dependent |
Dichte
POM has a density of approximately 1.40–1.43 g/cm³.
It is considerably lighter than aluminum while being significantly denser and stiffer than many commodity plastics.
This provides a useful combination of:
Typical unfilled POM provides tensile strength in the approximate range of 60–75 MPa, with tensile modulus commonly around 2.5–3.5 GPa.
This makes POM suitable for mechanically loaded components that would be too demanding for softer plastics such as polyethylene.
However, POM should not be considered a direct replacement for metals in heavily loaded or high-temperature applications.
Impact Resistance
POM has good toughness and can tolerate repeated mechanical loading better than many brittle plastics.
Its actual impact performance depends on:
Verschleißfestigkeit
Wear resistance is one of POM's most important engineering advantages.
POM is frequently selected for moving components because of its combination of:
It is commonly used in:
Bushings
Rollers
Gears
Guide blocks
Sliding components
Bearing cages
For extremely demanding tribological applications, specialized POM grades containing PTFE, silicone or other lubricating modifiers may be more appropriate.
Temperature Resistance
POM generally performs well in moderate-temperature mechanical applications.
A typical continuous operating range is approximately −40°C to +90/100°C, depending strongly on grade, load and environment.
Short-term exposure may be possible at higher temperatures, but continuous service conditions should be evaluated against the manufacturer's specification.
POM is therefore generally unsuitable for applications involving sustained temperatures approaching its melting range.
Moisture Absorption
POM has relatively low moisture absorption compared with many polyamides.
This is an important advantage for precision components because dimensional changes caused by ambient humidity are generally smaller than with materials such as PA6.
Nevertheless, moisture and temperature still need to be considered when extremely tight tolerances are required.
3. POM Chemical Properties
Chemical Composition
POM is based primarily on repeating oxymethylene (-CH₂-O-) units.
Unlike metallic materials, POM does not have an ASTM/UNS elemental alloy composition.
The exact formulation varies by manufacturer and grade.
Commercial POM may contain:
Therefore, the specific material datasheet should always be used when a component has critical chemical or mechanical requirements.
Chemische Beständigkeit
POM generally provides good resistance to many:
Hydrocarbons
Oils
Fuels
Alcohols
Weak acids
Weak alkalis
Many organic solvents
This chemical resistance contributes to its use in mechanical and fluid-handling components.
However, POM has important chemical limitations.
Strong acids and strong oxidizing agents can cause degradation.
POM should be evaluated carefully when exposed to:
Korrosionsbeständigkeit
POM does not corrode or rust like metallic materials.
This makes it attractive for applications where metal corrosion would be problematic.
However, "corrosion-free" does not mean chemically inert. Chemical attack can still cause:
UV-Widerstand
Standard POM is not naturally optimized for long-term outdoor UV exposure.
Prolonged sunlight can cause:
For outdoor applications, a UV-stabilized grade should be considered.
Welding & Bonding Compatibility
POM is relatively difficult to bond using conventional adhesives compared with ABS.
This is largely related to its low surface energy and chemical resistance.
Possible joining methods include:
For precision assemblies, mechanical joining is often preferred.|
4. POM CNC Machinability Analysis
Machining Difficulty: Easy
POM is one of the most machinable engineering plastics for CNC manufacturing.
Its excellent machinability is a major reason why POM is frequently selected for precision plastic components.
Compared with many softer thermoplastics, POM produces relatively predictable chips and can achieve good surface quality when properly machined.
Recommended Cutting Tools
Recommended tools include:
The most important factor is maintaining a sharp cutting edge.
Dull tools can create:
General CNC Cutting Parameter Guidance
Typical starting ranges for unfilled POM can be approximately:
Parameter | Typical Starting Range |
Cutting speed | ~200–500 m/min |
Feed per tooth | ~0.05–0.20 mm/tooth |
Coolant | Dry/air blast or suitable coolant |
Tool material | Carbide preferred |
Cutting approach | Sharp, positive cutting geometry |
Chip evacuation | Important |
These are starting ranges rather than fixed production parameters. The optimum cutting conditions depend on tool diameter, flute count, machine spindle speed, workpiece geometry and grade.
CNC Milling POM
POM is highly suitable for:
Pocket milling
Contouring
Slotting
Drilling
Threading
3D surface machining
Precision profiling
For complex geometries, 3-axis, 4-axis and 5-axis CNC machining can all be used.
For high-quality surfaces, a dedicated finishing pass is generally preferable to relying entirely on the roughing toolpath.
CNC Turning POM
POM is particularly suitable for CNC turning.
Common turned components include:
Bushings
Rollers
Spacers
Shafts
Sleeves
Sealing components
Precision rings
Sharp turning tools and adequate chip clearance are important for maintaining dimensional accuracy.
Drilling POM
POM can be drilled efficiently.
Potential issues include:
For deep holes, peck drilling or optimized chip evacuation can be beneficial.
Tapping & Threading
POM can be directly tapped and threaded.
For low-load applications, machined plastic threads can work well.
For frequent assembly/disassembly or higher loads, consider:
The choice depends on load, assembly frequency and environmental conditions.
Common POM CNC Machining Problems
1. Dimensional Expansion or Contraction
POM can change dimension with temperature.
During machining, excessive heat can cause the component to measure differently immediately after machining than after it has thermally stabilized.
Solutions:
Keep cutting heat under control
Use sharp tools
Avoid excessive rubbing
Allow parts to thermally stabilize before final inspection
Maintain controlled inspection temperature
2. Burrs
Burrs can occur around:
Holes
Slots
Sharp external edges
Intersecting features
Sharp tooling and optimized finishing passes can significantly reduce burr formation.
3. Thin-Wall Deformation
Although POM is relatively stiff for a thermoplastic, thin sections can still deform under clamping force.
Recommended approaches include:
4. Heat Buildup
POM has relatively low thermal conductivity.
If cutting heat is not removed efficiently, localized temperature increases can affect:
Dimensionsgenauigkeit
Oberflächengüte
Tool life
Edge quality
Air blast and efficient chip evacuation are often effective.
5. Stringy or Recut Chips
Improper cutting conditions can produce undesirable chips.
Solutions include:
Optimizing feed rate
Increasing chip evacuation
Using suitable flute geometry
Avoiding excessive rubbing
CNC Tolerance Capability
POM is particularly suitable for precision machining.
Under controlled conditions, CNC machining can achieve approximately ±0.02–0.05 mm on selected features.
However, this should not be interpreted as a universal tolerance capability.
For very tight tolerances, engineers should account for:
Part dimensions
Thermal expansion
Material grade
Stock stress
Fixture method
Machining sequence
Inspection temperature
·
For functional designs, GD&T should be used to identify which dimensions actually require tight control rather than applying unnecessarily tight tolerances across the entire drawing.
Surface Finish
CNC-machined POM can achieve good surface quality.
A typical machined surface may fall approximately within:
Ra 0.8–3.2 μm
depending on:
Tool geometry
Cutting speed
Feed
Finishing strategy
Machine condition
Part geometry
For functional sliding surfaces, consistency and dimensional control can be more important than simply minimizing Ra.
5. Typical POM Applications & Part Scenarios
Industrial Automation
POM is extensively used for:
Guide blocks
Rollers
Bushings
Conveyor components
Positioning components
Sliding plates
Custom fixtures
Its low friction and wear resistance make it especially suitable for moving mechanisms.
Robotik
CNC-machined POM can be used for:
Bushings
Spacers
Rollers
Cable-routing components
Low-load gears
Guide components
End-effector components
For high-load robot joints, metal or reinforced engineering plastics may be more appropriate.
Precision Machinery
POM is frequently used in:
Lager
Bushings
Gears
Cam followers
Guide rails
Rollers
Mechanical couplings
Its combination of machinability and dimensional stability makes it a strong candidate for precision mechanical components.
Automobilindustrie
Potential applications include:
Fuel-system components
Bushings
Gear components
Clips
Rollers
Guide components
Interior mechanisms
The exact grade must be selected according to temperature, fuel and chemical exposure.
Electrical & Electronics
POM can be used for:
Insulating components
Connector components
Precision spacers
Switch mechanisms
Mechanical supports
However, electrical applications requiring flame-retardant certification should use an appropriately certified grade rather than generic POM.
Medical & Laboratory Equipment
Suitable applications may include:
Medical applications require appropriate material certification and consideration of cleaning, sterilization and regulatory requirements.
Semiconductor & Automation Equipment
POM can be used for selected:
Mechanical guides
Positioning fixtures
Handling components
Insulating mechanical parts
Low-friction mechanisms
For environments requiring exceptionally low outgassing, high-temperature resistance or specific chemical compatibility, specialized materials may be preferable.
6. Our POM CNC Machining Advantages
Material Selection Support
We can help select between:
POM-H
POM-C
Standard acetal
Modified/lubricated POM
Glass-filled POM
Other engineering plastic alternatives
Material selection can be based on:
Load
Friction
Wear
Temperature
Chemical exposure
Dimensional requirements
Produktionsvolumen
Mature CNC Process Control
POM is highly machinable, but precision results still depend on process engineering.
Our process planning considers:
This is particularly important for precision gears, bushings and thin-wall components.
High-Precision CNC Machining
For critical POM components, we can control:
Bore diameter
Shaft diameter
Konzentrizität
Ebenheit
Parallelismus
Position
Profile
Thread dimensions
GD&T requirements can be incorporated directly into the manufacturing and inspection process.
Prototype to Batch Production
POM CNC machining can support:
One-off engineering parts
Prototype components
Low-volume production
Pilot runs
Repeated batch production
Higher-volume CNC manufacturing
For larger quantities, machining strategy and nesting can be optimized to improve material utilization and reduce cycle time.
Surface & Post-Machining Services
Depending on application requirements, post-processing can include:
Precision deburring
Edge breaking
Polieren
Cleaning
Laser marking
Part identification
Montage
Because POM has low surface energy and good chemical resistance, finishing processes should be selected specifically for the material.
Quality Inspection & Material Documentation
Inspection can include:
Dimensional inspection
GD&T verification
Bore and thread inspection
Surface-finish inspection
Visual inspection
Critical-feature inspection
Material documentation where available
For production orders, inspection requirements can be established according to the customer's drawing and quality specifications.
POM CNC Machining Material Selection Summary
Requirement | POM Suitability |
CNC Fräsen | Ausgezeichnet |
CNC Drehen | Ausgezeichnet |
Drilling | Ausgezeichnet |
Thread machining | Ausgezeichnet |
Präzisionsbearbeitung | Ausgezeichnet |
Gear machining | Ausgezeichnet |
Bushing machining | Ausgezeichnet |
Low-friction components | Ausgezeichnet |
Wear resistance | Ausgezeichnet |
Dimensional stability | Ausgezeichnet |
Moisture resistance | Gut |
Chemische Beständigkeit | Gut |
High-temperature applications | Limited–Moderate |
UV-Beständigkeit | Limited for standard grades |
Adhesive bonding | Schwierig |
Lightweight applications | Gut |
High-load structural components | Gemäßigt |
Cost efficiency | Gut |
POM vs. ABS for CNC Machining
Charakteristisch | POM | ABS |
Bearbeitbarkeit | Ausgezeichnet | Ausgezeichnet |
Stiffness | Höher | Gemäßigt |
Wear resistance | Höher | Gemäßigt |
Friction | Niedriger | Höher |
Dimensional stability | Ausgezeichnet | Gut |
Impact resistance | Gut | Ausgezeichnet |
Chemische Beständigkeit | Gut | Gemäßigt |
Moisture absorption | Very low | Niedrig |
Cosmetic appearance | Gut | Ausgezeichnet |
Adhesive bonding | Schwierig | Easier |
Typical mechanical parts | Ausgezeichnet | Gut |
Housings/enclosures | Gut | Ausgezeichnet |
Gears/bushings | Ausgezeichnet | Limited |
Relative material cost | Gemäßigt | Niedrig |
Final Engineering Recommendation
POM/Delrin is one of the strongest choices for CNC machined plastic components that require precision, low friction, wear resistance and dimensional stability. It is particularly well suited to gears, bushings, rollers, spacers, guide components and other moving mechanical parts.
For procurement engineers and designers, the most important specification is not simply "Delrin." The drawing or purchase specification should identify the required POM grade, mechanical requirements, operating temperature, chemical environment, dimensional tolerances and any applicable certifications.
Contact us for a CNC machining quote and DFM consultation for POM/Delrin parts, including material-grade selection, precision machining, tolerance review and batch-production planning.
Erhalten Sie ein sofortiges Angebotfür Ihre kundenspezifischen POM-C Teile heute.