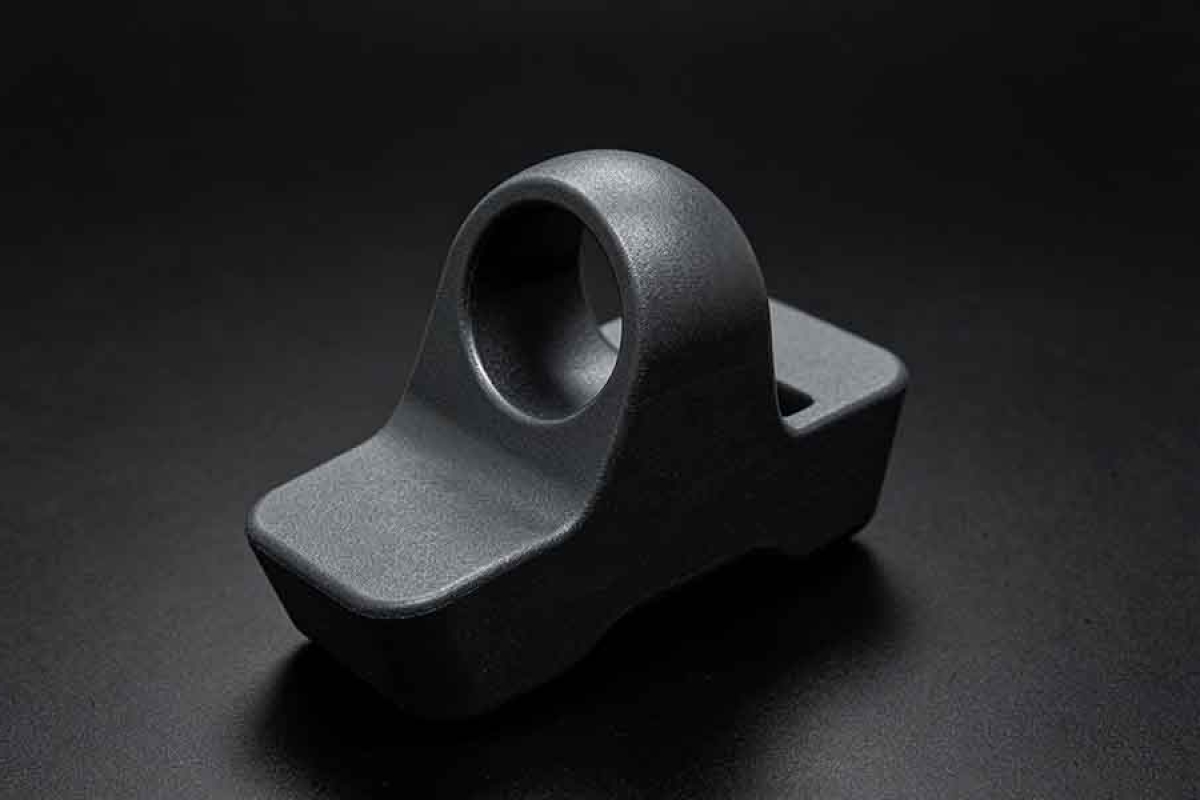
Material de mecanizado CNC PPS (Sulfuro de polifenileno)
PPS (Polyphenylene Sulfure) es un termoplástico de ingeniería de alto rendimiento ampliamente utilizado para componentes mecanizados CNC de precisión que requieren una excelente resistencia química, estabilidad dimensional, baja absorción de humedad, aislamiento eléctrico y rendimiento a temperaturas elevadas.
1. Información material básica
¿Qué es PPS?
El PPS, o sulfuro de polifenileno, es un termoplástico de ingeniería de alto rendimiento conocido por su excelente estabilidad dimensional, resistencia química, baja absorción de humedad, propiedades de aislamiento eléctrico y resistencia a temperaturas elevadas.
Para el mecanizado CNC, PPS es particularmente valioso para componentes de precisión que requieren una combinación de baja sensibilidad a la humedad, estabilidad térmica, aislamiento eléctrico y resistencia a productos químicos agresivos.
El material de mecanizado de PPS está disponible en diferentes formulaciones, incluyendo PPS sin rellenar, PPS reforzado con fibra de vidrio, PPS lleno de minerales y PPS modificado con lubricante. Las propiedades exactas y la mecanizabilidad dependen del grado del fabricante seleccionado.
Designaciones estándar e identificación del material
Artículo | Designación típica |
|---|
Material | Sulfuro de polifenileno |
Abreviatura | PPS |
Familia de polímeros | Termoplástico de ingeniería de alto rendimiento |
Descripción común | PPS, PPS lleno de vidrio, PPS reforzado |
Designación de material ISO | PPS |
Clasificación ASTM | ASTM D4067 para compuestos de moldeo y extrusión de PPS |
Stock de mecanizado | Hoja, placa, varilla, tubo y stock personalizado |
Grado reforzado común | PPS GF30 / PPS reforzado con fibra de vidrio al 30% |
Material Grade Note: PPS is a polymer family rather than one single universal grade. Mechanical properties, temperature capability, dimensional stability, and machinability vary between unfilled and reinforced formulations. Always verify the manufacturer's technical data sheet before approving material substitutions.
Posicionamiento del mercado principal
PPS occupies the high-performance engineering thermoplastic segment between conventional engineering plastics and ultra-high-performance materials such as PEEK and PAI.
Excellent chemical resistance
Very low moisture absorption
Excellent dimensional stability
High thermal resistance
Strong electrical insulation performance
Good flame resistance in many formulations
Low creep compared with many conventional thermoplastics
Good wear performance when properly compounded
2. Physical Properties of PPS
The following values represent typical ranges for representative PPS materials rather than guaranteed specifications. Actual properties depend on resin formulation, reinforcement, processing history, and supplier grade.
Propiedad | Valor típico / Rango |
|---|
Density, unfilled PPS | ~1.35 g/cm³ |
Density, glass-filled PPS | ~1.60–1.70 g/cm³ |
Tensile Strength, unfilled | ~60–90 MPa |
Tensile Strength, GF-reinforced | ~100–200+ MPa |
Tensile Modulus, unfilled | ~3–4 GPa |
Tensile Modulus, reinforced | ~7–15 GPa |
Elongación en el descanso | Typically ~1–5% |
Módulo Flexible | Grade dependent |
Dureza | Grade dependent |
Absorción de agua | Muy bajo |
Temperatura de fusión | Approximately 280–290°C |
Glass Transition Temperature | Approximately 80–90°C |
Conductividad térmica | Approximately 0.2–0.5 W/m·K, formulation dependent |
Service Temperature | Commonly 200°C-class applications; grade dependent |
aislamiento eléctrico | Excellent in many grades |
Estabilidad dimensional
One of the biggest advantages of PPS for precision CNC machining is its very low moisture absorption. Compared with moisture-sensitive engineering plastics such as nylon, PPS maintains much more stable dimensions under changing humidity conditions.
This makes PPS suitable for precision electrical components, semiconductor equipment components, fluid-handling parts, instrumentation components, and precision fixtures.
Resistencia a la temperatura
PPS maintains useful mechanical and dimensional performance at temperatures significantly above those tolerated by many conventional thermoplastics. However, the actual service temperature must be verified for the specific PPS grade and operating environment.
Wear and Friction
Unfilled PPS provides useful wear resistance, while specialized filled PPS grades can provide substantially better tribological performance. Common modifications include glass fiber, carbon fiber, PTFE, and graphite.
3. Chemical Properties of PPS
Resistencia química
PPS is one of the strongest engineering plastics when chemical resistance is a primary design requirement. It demonstrates excellent resistance to many acids, alkalis, hydrocarbons, fuels, oils, solvents, cleaning chemicals, detergents, and industrial fluids.
Chemical compatibility should always be evaluated against the specific chemical, concentration, temperature, exposure time, and mechanical loading condition.
Oxidación y estabilidad ambiental
PPS has strong resistance to thermal and oxidative aging compared with many conventional thermoplastics. Its low moisture uptake also helps maintain dimensional stability in humid environments.
For outdoor applications, weathering resistance depends on formulation, additives, pigmentation, and UV exposure. A UV-stabilized grade may be preferable for long-term outdoor use.
Composición química
PPS consists primarily of repeating phenylene-sulfide units, with carbon, hydrogen, and sulfur forming the polymer backbone. Commercial PPS compounds may also contain glass fiber, carbon fiber, mineral reinforcement, PTFE, graphite, flame-retardant systems, and processing modifiers.
Welding and Bonding Compatibility
PPS can be joined using specialized thermoplastic joining methods. Depending on the grade and design, possible joining methods include mechanical fastening, thermal welding, ultrasonic welding, and specialized adhesive bonding.
4. CNC Machinability Analysis of PPS
PPS CNC Machining Difficulty: Moderate
PPS is machinable using conventional CNC equipment, but precision machining requires better process control than machining common plastics such as ABS or POM.
Common machining challenges include heat accumulation, material deflection, burr formation, fiber pull-out in reinforced grades, edge chipping, dimensional variation, and surface damage caused by excessive cutting temperature.
Unfilled PPS vs. Glass-Filled PPS
Unfilled PPS | Glass-Filled PPS |
|---|
Easier to machine | Mayor rigidez |
Lower tool wear | Higher tool wear |
Better tool life | Mejor estabilidad dimensional |
Lower stiffness | Greater risk of fiber exposure |
Potential deflection during aggressive machining | Requires more wear-resistant tooling |
Recommended CNC Cutting Tools
Sharp carbide tooling is generally suitable for unfilled PPS. For reinforced PPS, particularly glass-filled grades, wear-resistant carbide tooling is strongly preferred. Diamond tooling can be considered for high-volume production where extended tool life and consistent surface quality justify the tooling investment.
General CNC Machining Parameter Starting Points
Operation | Starting Consideration |
|---|
fresado | Moderate-to-high cutting speed with sharp carbide tooling |
Rough Milling | Conservative feed with effective chip evacuation |
Finish Milling | Reduced radial engagement and sharp cutting edges |
Drilling | Sharp drill, controlled feed, frequent chip evacuation |
Tapping | Lower cutting load and careful chip evacuation |
Girando | Sharp positive-rake carbide tooling |
Reaming | Controlled feed and sufficient chip clearance |
Process Note: Cutting parameters should be validated against the actual PPS grade, tool geometry, tool diameter, machine rigidity, workholding method, and production requirements. The values above are process-development starting points rather than universal production parameters.
Common PPS CNC Machining Problems and Solutions
1. Burr Formation
Dull tools, excessive feed, unsuitable tool geometry, and insufficient support can cause burrs. Use sharp tooling, optimize feed rate, select appropriate cutting geometry, and apply controlled deburring.
2. Fiber Pull-Out in GF PPS
Use sharp carbide tooling, minimize tool deflection, use controlled finishing passes, avoid excessive tool wear, and optimize cutting direction and tool engagement.
3. Dimensional Deviation
Thin-wall deflection, excessive clamping force, machining heat, residual stress, and tool deflection can all contribute to dimensional deviation. A controlled sequence of roughing, stress relaxation where appropriate, semi-finishing, finishing, and inspection can improve consistency.
4. Edge Chipping
Sharp internal corners and unsupported small features can chip during machining. Where functional requirements allow, use appropriate internal radii and provide adequate material support.
5. Surface Smearing
Surface smearing can indicate excessive heat or poor tool condition. Check tool sharpness, reduce heat generation, improve chip evacuation, adjust cutting engagement, and use a dedicated finishing tool.
PPS CNC Machining Tolerances
CNC machining of PPS can achieve tight dimensional tolerances, but the practical tolerance depends on part size, wall thickness, geometry, reinforcement, clamping, thermal conditions, machine capability, and inspection method.
For many precision PPS components, approximately ±0.05 mm can be a practical engineering target on suitable dimensions and geometries. Tighter tolerances may require specialized process control and inspection.
Tratamiento de superficie
With appropriate tooling and finishing parameters, machined PPS can achieve a smooth surface. A typical CNC-machined surface may be approximately Ra 1.6–3.2 μm, with finer finishes possible under optimized conditions.
5. PPS CNC Machining Processes
Fresado CNC
PPS is suitable for 3-axis CNC milling, 4-axis machining, and 5-axis machining. Five-axis machining is especially useful for complex PPS components requiring multiple angled surfaces, deep features, or reduced repositioning.
Typical parts include housings, brackets, insulators, fixtures, manifolds, pump components, and semiconductor equipment parts.
Torneado CNC
PPS rods and tubes can be CNC turned into bushings, sleeves, seals, rings, spacers, valve components, and precision cylindrical components.
CNC Drilling
PPS can be drilled using carbide or suitable high-speed tooling. For deep holes, effective chip evacuation is especially important to prevent excessive heat accumulation.
CNC Tapping
PPS can be tapped, but thread geometry and wall thickness should be carefully considered. For highly loaded or repeatedly assembled components, threaded inserts may provide better long-term thread durability.
molienda
Grinding can be used where tighter dimensional control or specialized surface requirements are necessary. Thermal management remains important because PPS has relatively low thermal conductivity.
6. PPS for Thin-Walled and Complex CNC Parts
PPS is attractive for precision complex parts because its low moisture absorption helps maintain dimensional stability. However, thin-wall machining remains challenging.
Recommended Process Strategy
Use sufficient stock during roughing.
Avoid excessive clamping pressure.
Leave controlled finishing allowance.
Use sharp finishing tools.
Minimize heat accumulation.
Finish critical surfaces in a stable thermal condition.
Inspect after the part has reached a stable temperature.
For reinforced PPS, the machining process should additionally account for fiber orientation, fiber exposure, and abrasive tool wear.
7. Typical PPS Applications and Part Scenarios
Semiconductor Equipment
PPS is well suited to semiconductor manufacturing equipment because of its low moisture absorption, chemical resistance, dimensional stability, electrical insulation, and thermal resistance.
Electrical and Electronics
Automotriz
PPS can be used in demanding automotive environments where resistance to heat, fluids, and chemicals is required.
Sensor components
Pump components
Componentes de válvula
Electrical housings
Fuel-system components
Under-hood components
Chemical Processing
Industrial Automation
Medical and Laboratory Equipment
Selected PPS grades can be suitable for precision laboratory and equipment components where chemical resistance and dimensional stability are important. Medical suitability, sterilization resistance, and regulatory compliance must be verified against the specific grade and application.
8. PPS vs. Other CNC Machining Plastics
Propiedad | PPS | PEEK | POM | Nylon |
|---|
Resistencia a la temperatura | Sobresaliente | Sobresaliente | Moderado | Moderado |
Resistencia química | Sobresaliente | Sobresaliente | Bueno | Moderado |
Moisture Absorption | Very Low | Very Low | Bajo | Más alto |
Estabilidad dimensional | Sobresaliente | Sobresaliente | Bueno | Moderado |
Resistencia al desgaste | Bueno-Excelente | Sobresaliente | Sobresaliente | Bueno |
Resistencia al impacto | Moderado | Sobresaliente | Bueno | Bueno |
Machinabilidad CNC | Moderado | Moderado | Easy | Easy–Moderate |
Relative Material Cost | Alto | Very High | Más abajo | Más abajo |
aislamiento eléctrico | Sobresaliente | Sobresaliente | Bueno | Bueno |
PPS vs. PEEK
PEEK generally offers superior mechanical performance and broader high-temperature capability, while PPS can provide an attractive balance of chemical resistance, dimensional stability, electrical performance, and material cost.
PPS vs. POM
POM is generally easier and less expensive to machine. PPS becomes more attractive when the component must tolerate higher temperatures or aggressive chemical environments.
PPS vs. Nylon
PPS has a major advantage in moisture stability and high-temperature chemical resistance. Nylon may be preferable when toughness, impact resistance, or lower material cost is more important.
9. Our PPS CNC Machining Advantages
Material Selection Support
We can help determine whether the application requires unfilled PPS, glass-filled PPS, carbon-filled PPS, PTFE-modified PPS, or another wear-modified formulation.
Material selection should be based on temperature, load, chemical exposure, friction, electrical requirements, and dimensional tolerances.
Proven CNC Process Development
Tool selection
Cutting-condition development
Workholding strategy
Heat management
Roughing and finishing sequence
Burr control
Dimensional compensation
Batch consistency control
Precision Inspection
Critical PPS components can be inspected using appropriate dimensional inspection equipment and documented against engineering drawings and GD&T requirements.
Informes de inspección dimensional
Inspección del primer artículo (FAI)
Material certificates / MTR documentation when available
Certificate of Conformance
Surface-finish verification where specified
Prototype to Batch Production
PPS CNC machining can support engineering prototypes, low-volume production, pilot production, and repeat batch manufacturing. Production processes can be optimized as quantities increase through improved fixtures, tooling, machining parameters, inspection methods, and cycle-time control.
10. PPS CNC Machining Design Guidelines
Avoid Extremely Thin Walls
Very thin sections are more susceptible to machining deflection and clamping distortion.
Add Internal Radii
Where functionally acceptable, internal radii reduce stress concentration and make milling more stable.
Consider Threaded Inserts
For frequently assembled components, threaded inserts can provide improved thread durability compared with repeatedly loading machined polymer threads.
Define Functional Tolerances
Avoid specifying unnecessarily tight tolerances on every dimension. Apply tighter tolerances only where component interfaces and functional requirements demand them.
Identify the Exact PPS Grade
Production drawings should identify the resin family, reinforcement percentage, manufacturer grade when required, color where relevant, regulatory requirements, and mechanical or thermal requirements.
11. PPS CNC Machining FAQ
Is PPS easy to CNC machine?
PPS is generally considered moderately machinable. Unfilled PPS is easier to machine, while glass-filled and other reinforced grades require greater attention to tool wear and surface quality.
Can PPS be CNC milled?
Yes. PPS can be CNC milled using sharp carbide tooling and appropriate heat-management strategies.
Can PPS be CNC turned?
Yes. PPS rods and tubes can be CNC turned for bushings, sleeves, rings, spacers, and other precision cylindrical components.
Is PPS better than PEEK?
Not universally. PEEK generally provides higher overall mechanical performance, while PPS can offer an attractive combination of chemical resistance, dimensional stability, electrical insulation, and cost.
Is PPS suitable for high-temperature applications?
Yes. PPS is widely used in high-temperature engineering applications, but the actual continuous-use temperature must be confirmed for the selected grade and service conditions.
Can PPS be used for semiconductor equipment?
Yes. Its low moisture absorption, chemical resistance, dimensional stability, and electrical properties make suitable PPS grades valuable for semiconductor equipment components.
Does glass-filled PPS require special CNC tooling?
Glass-filled PPS benefits from wear-resistant tooling because glass fibers are abrasive. Tool wear should be monitored carefully during batch production.
12. Conclusion: PPS for Precision CNC Machining
PPS (Polyphenylene Sulfide) is a high-performance engineering thermoplastic that combines excellent chemical resistance, low moisture absorption, strong dimensional stability, thermal resistance, and electrical insulation performance.
For CNC machining, PPS is particularly suitable for precision components used in semiconductor equipment, automotive systems, electrical and electronics, chemical processing, industrial automation, laboratory equipment, and other demanding industrial applications.
The key to successful PPS machining is the complete manufacturing process, including material grade selection, tooling, workholding, heat management, machining sequence, dimensional compensation, and inspection.
For glass-filled PPS, additional attention should be given to tool wear, fiber exposure, surface quality, and production consistency.
Request a PPS CNC Machining Quote
Contact us for a CNC machining quote and DFM consultation for your PPS parts. We can review your drawings, material grade, tolerances, surface-finish requirements, and production volume to develop a practical machining and manufacturing solution.
Solicitar un presupuesto instantáneopara sus piezas PPS personalizadas hoy.